
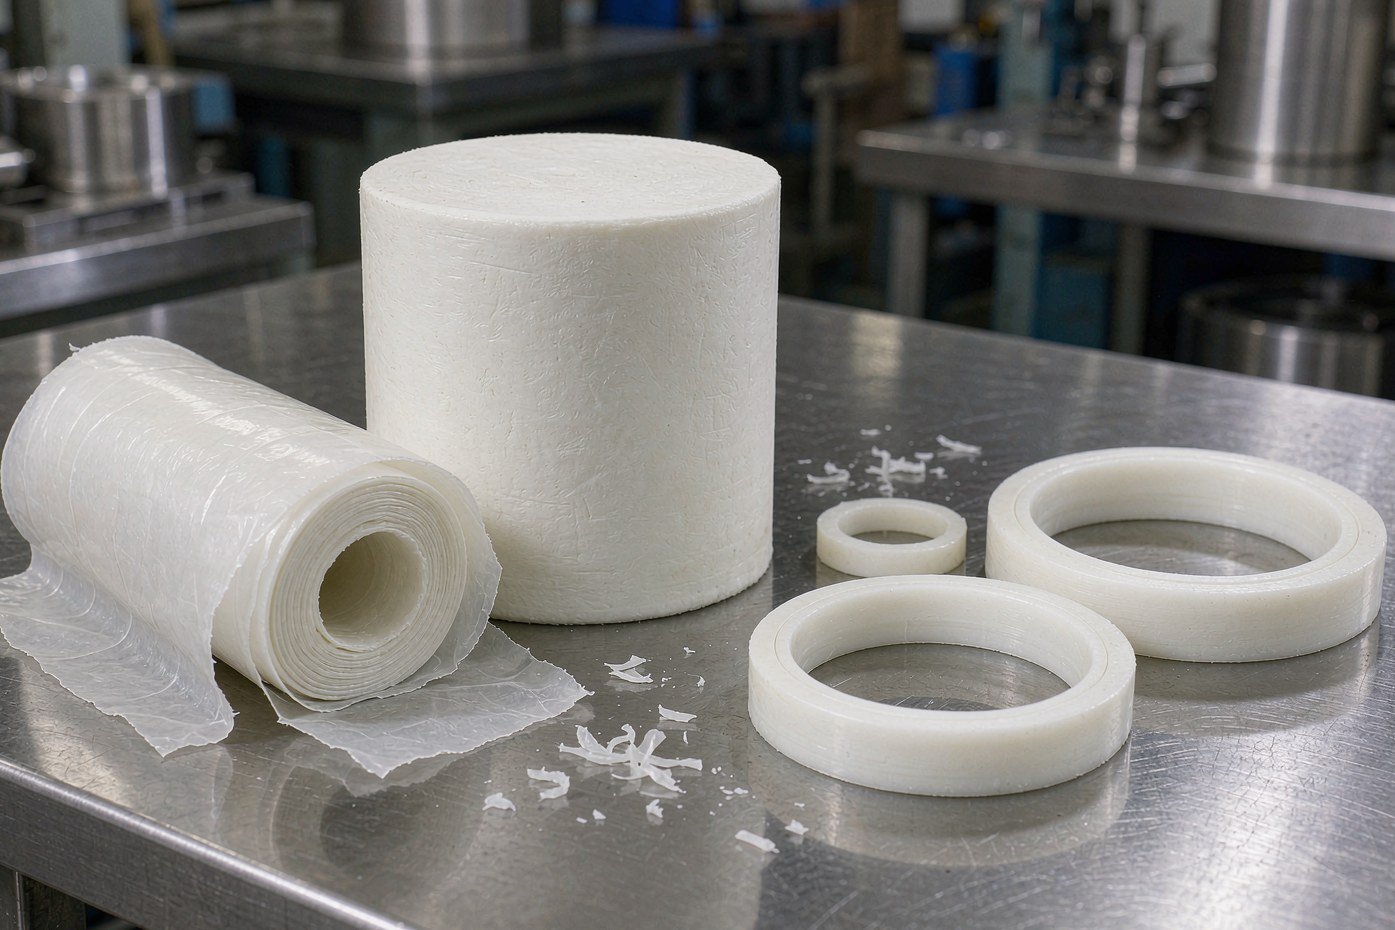
Ask three seal buyers what they mean by “virgin PTFE” and you get three different answers. One means unfilled. One means not reprocessed. One means the part was machined from a moulded billet rather than punched from skived film. All three are legitimate, and none of them is the same decision as the other two.
PTFE is not injection moulded, so every PTFE seal carries the fingerprint of how it was made: the sintering cycle, the direction the material was cut, the filler and its percentage, and whether the powder was virgin or regrind. Those four variables move creep, wear and elongation by more than most buyers expect. This is what each one actually changes.
There Is No Such Thing as Cast PTFE
The trade says “cast PTFE” for what the standard calls compression moulded and sintered. The powder is pressed cold into a preform — commonly 20–35 MPa — then heated above its crystalline melting point of about 327 °C and held, usually at 360–380 °C, until the particles coalesce. There is no liquid phase and no flow. Above the melting point the melt viscosity is on the order of 1011 poise, which is why PTFE behaves more like a sintered metal than a mouldable plastic.
Everything else follows from that. Because the material cannot be melted and re-formed, parts are either moulded near-net and finished, or machined from a billet, rod or tube. Because it cannot be welded or reprocessed by melting, scrap is ground and sold as repro — a real cost saving and a real change in properties.
| Route | How the shape is made | Typical products | What it does to the material |
|---|---|---|---|
| Compression moulding + sintering | Cold preform, free sinter at 360–380 °C | Billets, large sheets, near-net rings | Most uniform; properties depend on heating and cooling rate |
| Skiving | Peeling a thin layer off a moulded billet on a lathe | Film, sheet, thin back-up rings, gaskets | Adds orientation along the cut; lower elongation across it |
| Ram extrusion | Pre-sintered powder forced through a heated die | Rod, heavy-wall tube | Longitudinal orientation; diameter-limited; stress varies across the section |
| Isostatic moulding | Powder compacted evenly under fluid pressure, then sintered | Large or thick near-net shapes, big valve seats | Even density in all directions; closest to isotropic |
| Paste extrusion | Fine powder plus a hydrocarbon aid, extruded, dried, sintered | Thin-wall tube, tape, cord | Lowest mechanical strength; used where thin sections are needed |
Notice what is missing: no injection moulding, no blow moulding, no melt welding. If a supplier offers a “cast” PTFE seal with a complex moulded rib in one shot, ask which polymer it actually is, because PFA and FEP can be injection moulded and PTFE cannot.
Sintering Is Where the Crystallinity Is Set
The sintering cycle is not a formality that only affects colour. It sets the degree of crystallinity, and crystallinity sets stiffness, elongation and creep.
ASTM D4894 tabulates the reference cycles for test specimens: initial hold at 238 °C or 290 °C, heating at 60 °C/h or 120 °C/h, a hold at 357–380 °C for 30 minutes to 16 hours depending on section, then cooling at 60 °C/h. Those numbers exist because the result depends on them.
Cool slowly and the polymer chains have time to order themselves: crystallinity ends up higher, the part is stiffer and stronger in compression, and elongation drops. Cool fast and crystallinity falls: the part is tougher, more forgiving of impact, and creeps more under sustained load.
For a seal this is a real design choice, not a manufacturing detail. A back-up ring that has to hold 35 MPa without cold-flowing wants the slow-cooled, higher-crystallinity structure. A thin lip that has to survive handling and installation without cracking wants the faster-cooled, tougher structure. Two parts with the same drawing and the same resin can behave differently because the oven cycle differed, and the drawing usually says nothing about it.
Skived or Machined: the Direction of the Grain
Skiving peels a continuous film off a rotating billet, like unrolling a very stiff tape. The process imposes orientation along the cut direction. Along that direction the material is strong; across it, elongation is lower and a thin ring is more likely to split at a stress point.
Machining removes material instead, and leaves the crystalline structure largely as the billet had it, with machining stress near the surface. For a ring of 3 mm wall or more, machining gives a more predictable part. For thin sections below about 2 mm — the classic back-up ring, flange gasket or diaphragm — skiving is the only economical route, and the orientation becomes something the designer has to live with.
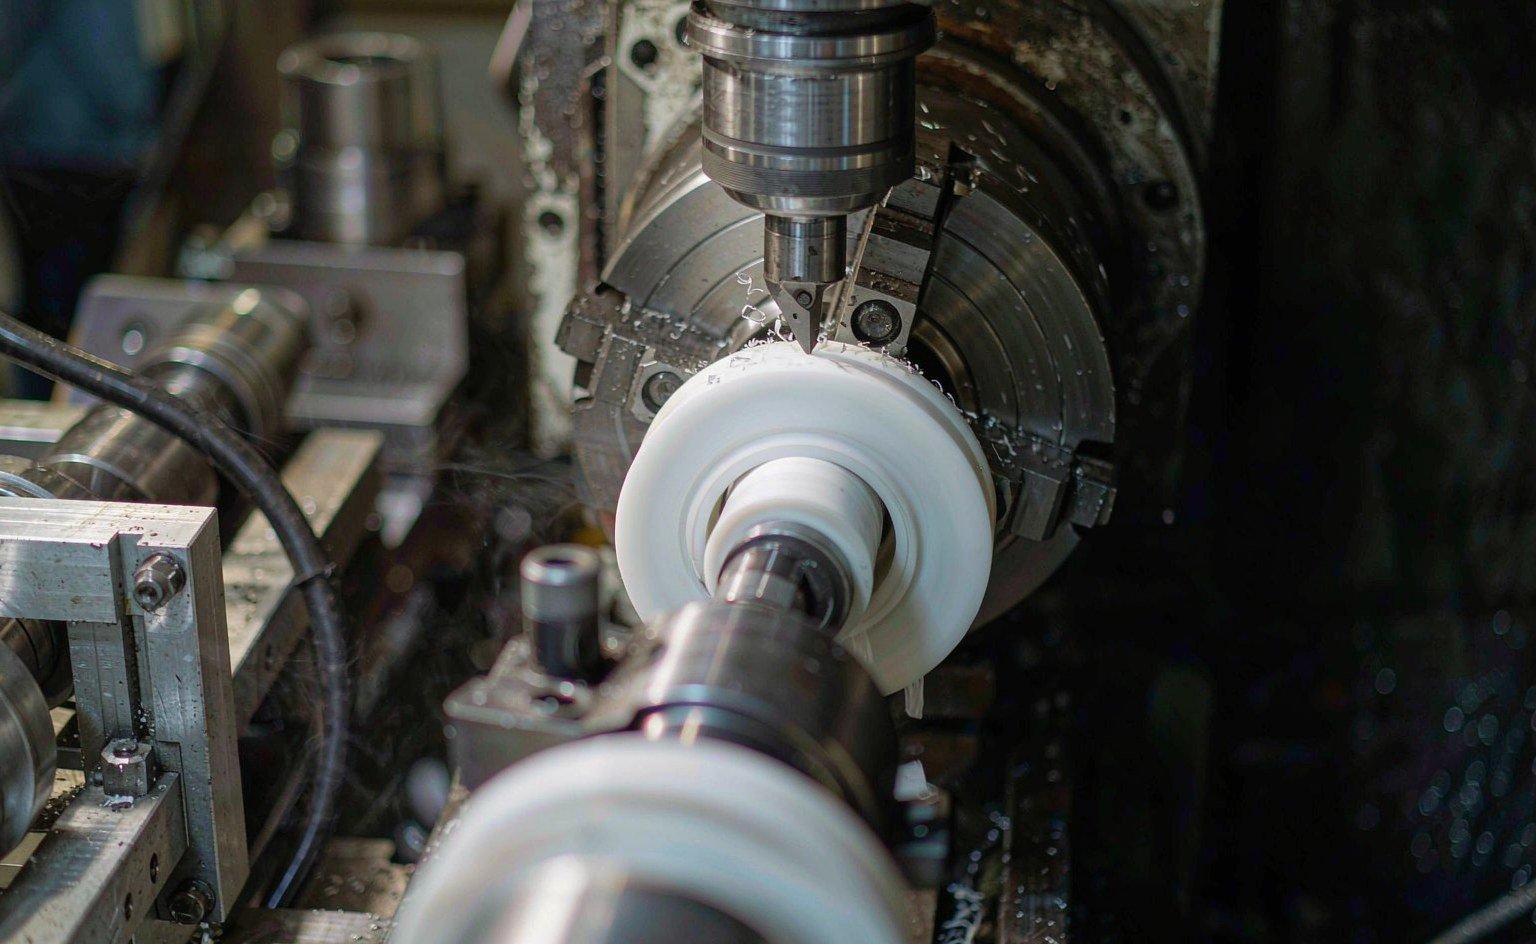
Two practical consequences. First, a skived back-up ring should be installed so that its cut direction runs circumferentially, not radially, or the scarf joint becomes a leak path. Second, thin skived rings have a thickness tolerance that is a percentage of the skived thickness, not an absolute number, so a 0.5 mm ring is proportionally much less precise than a 2 mm one. If a groove needs 0.05 mm accuracy, specify machined.
Virgin, Repro, or Filled
Three different words that get used interchangeably in quotations, and they are not interchangeable.
Virgin means new powder. Repro means ground sintered scrap, blended back at some percentage. Filled means an additive — glass, carbon, graphite, bronze, moly, PEEK — blended into virgin powder before sintering. Repro lowers cost and lowers, and destabilises, elongation and dielectric strength; it is the one that matters most for food, pharma and electrical parts. Filled changes mechanical behaviour on purpose.
| Propiedad | PTFE virgen | 15–25% glass filled | Carbon / graphite filled | Bronze filled |
|---|---|---|---|---|
| Specific gravity | 2.14–2.16 | 2.20–2.25 | 2.10–2.15 | 3.7–4.0 |
| Resistencia a la tracción | 25–38 MPa | 15–20 MPa | 15–20 MPa | 13–18 MPa |
| Alargamiento a la rotura | 300–400% | 200–250% | 100–150% | 100–150% |
| Deformation under load, 15 MPa / 24 h | About 16% | 6–10% | 6–10% | 3–5% |
| Thermal conductivity | 0.22–0.25 W/m·K | 0.35–0.45 | 0.5–0.8 | 1.5–2.0 |
| Resistencia química | Full | Except HF and hot caustic | Full to most media | Poor in acids |
Values are typical for commercial grades; confirm them on the grade data sheet. Note also how sharply the mechanical properties fall with temperature — published PTFE property tables show flexural modulus dropping from roughly 650 MPa at room temperature to about 45 MPa at 260 °C. A part rated for 260 °C is not a part that can carry the same load at 260 °C.
The deformation row is the one that decides seal designs. Virgin PTFE at 15 MPa loses about a sixth of its thickness in a day under load. That is cold flow, and it is why a virgin PTFE back-up ring in a 35 MPa gland will extrude out of the gap no matter how well it was machined. A glass- or carbon-filled grade cuts that deformation by roughly two-thirds, at the cost of elongation and, for glass, resistance to hydrofluoric acid and strong caustic.
Our own rule of thumb: virgin PTFE for chemical inertness and gaskets, glass or carbon filled for back-up rings and wear parts under load, bronze only where thermal conductivity matters more than corrosion. Above about 40 MPa PEEK often wins on creep regardless of filler, and this walk-through of PTFE gasket manufacturing shows the same processing trade-offs on a simpler part.
What the Certificate Should Prove
Three numbers on a material certificate tell you more than any brochure claim.
Standard specific gravity (SSG). Measured per ASTM D4894, it sits around 2.14–2.16 for virgin granular PTFE. A value outside that band suggests filler, repro content, or a different resin type — and it is the fastest way to catch a substitution.
Tensile strength and elongation. Measured on standard specimens, typically 25–38 MPa and 300–400% for virgin moulded PTFE. Low elongation with normal SSG points to over-sintering or excessive repro content; low tensile with high SSG points to filler.
Filler content and type. Ask for the percentage and the tolerance, not just “glass filled”. A 15% glass grade and a 25% glass grade are different products with different wear and different machining behaviour.
The standards worth naming on a purchase order: ASTM D4894 for granular moulding and ram extrusion resin, ASTM D4895 for fine powder, and ASTM D1710 for extruded rod and heavy tube. For semi-finished shapes, ISO 13000 covers the same ground internationally.
Where Processing Shows Up in the Field
Most “PTFE failed” reports we receive trace back to one of five causes, and only one of them is the polymer itself.
| What the customer sees | Likely processing cause | Qué cambiar |
|---|---|---|
| Ring extruded into the gap, cracked at the back edge | Virgin or lightly filled grade in a high-pressure gland | Filled PTFE or PEEK; reduce gap; support both sides |
| Thin ring split at installation | Skived film loaded across its orientation, or too little elongation | Rotate the cut, increase thickness, or switch to machined |
| Part measures undersize after a month in service | Cold flow, not wear | Filled grade, lower surface pressure, or a spring-energized design |
| White powder or flaking on a food line | Repro content or contaminated regrind | Virgin, food-contact grade with a written declaration |
| Cracks radiating from the bore after sintering | Heating or cooling too fast for the section, uneven preform density | Cycle per D4894 reference table; check preform pressure |
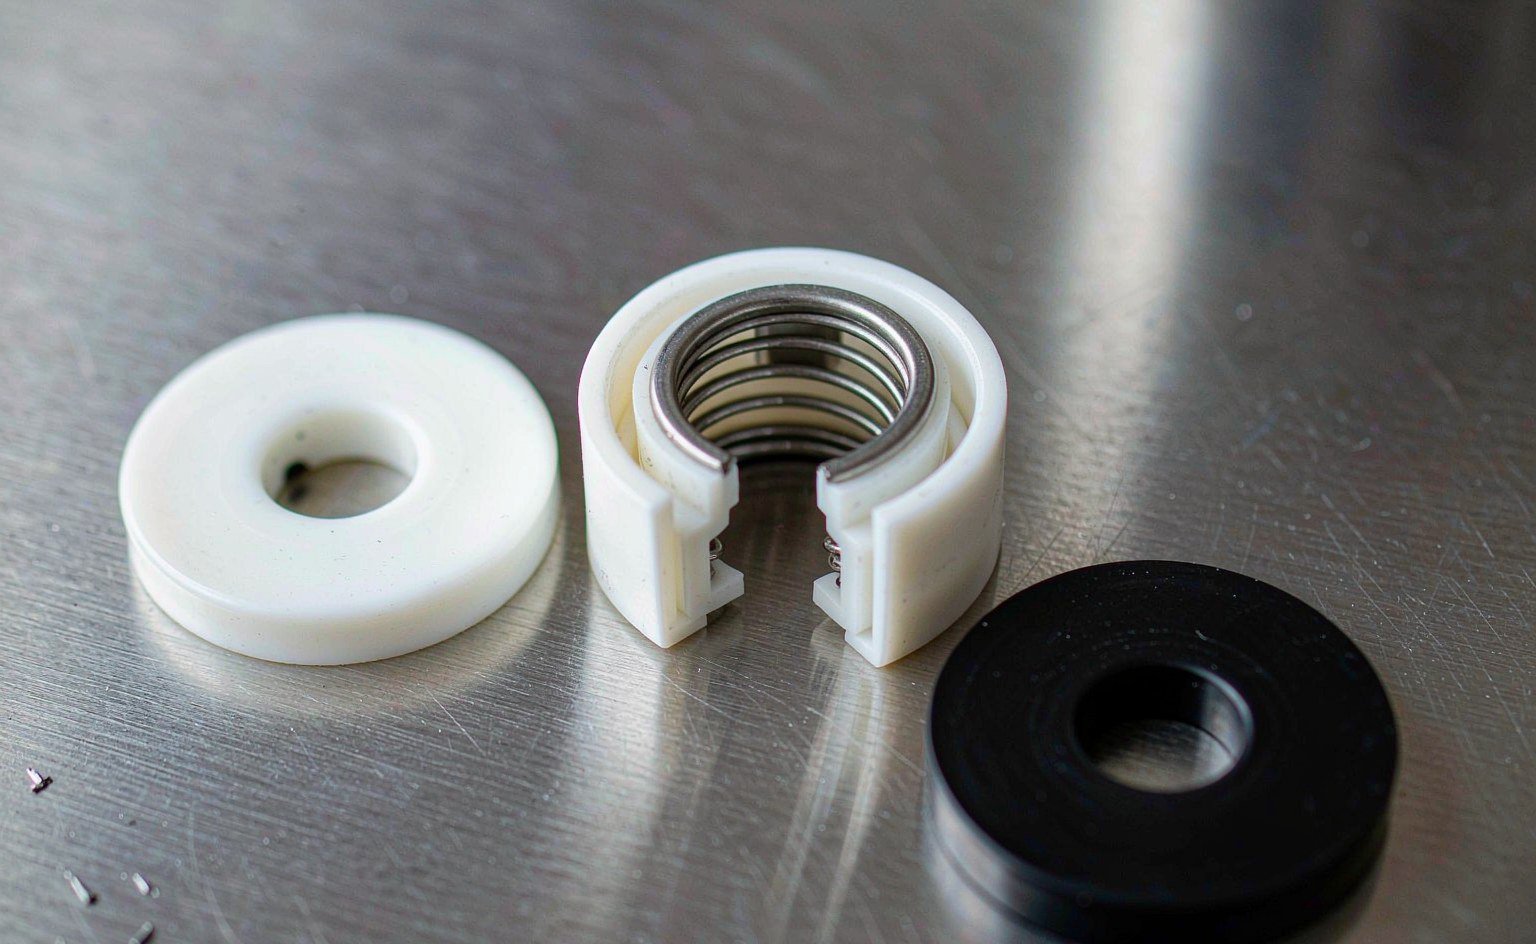
The first row accounts for most of the failures. A designer picks virgin PTFE because it is the most chemically inert option, then puts it in a 35 MPa gland with a 0.4 mm clearance and expects it to behave like an elastomer. It will not. PTFE seals need a support strategy — a closed groove, a filled grade, or a spring — because the material has no elastic memory to recover from deformation. This material guide y this PTFE reference both state the filler-versus-service trade-off plainly, if you want a second source before a design review.
What to Write on the Purchase Order
Five lines, and the argument about “virgin PTFE” disappears:
- Resin type and standard — granular per ASTM D4894, or fine powder per D4895, with SSG range.
- Filler type and percentage, with the tolerance you accept.
- Form — moulded near-net, machined from billet, or skived film, with the thickness tolerance as an absolute value.
- Sintering requirement if the part is load-bearing: crystallinity target or a cooling rate, not just “sintered”.
- Virgin or repro, stated explicitly, plus the food-contact or PFAS declaration your customer needs.
If you cannot get lines 1 to 5, you are buying a shape, not a material. For back-up rings and gaskets that may be fine. For a seal that holds pressure at temperature for a decade, it is the difference between a specification and a hope.
La conclusión
PTFE processing is not a commodity detail. Sintering sets crystallinity and therefore creep; skiving sets orientation and therefore where a thin ring will split; the filler decides whether a back-up ring holds 35 MPa or flows out of the groove; and virgin versus repro decides whether the part belongs near food.
For a buyer, the practical sequence is short. Decide whether the part needs inertness or load capacity, because those pull in opposite directions. Then pick the forming route that matches the section thickness — machined above 2–3 mm, skived below. Then write the material standard and the filler percentage on the order, and ask for SSG and elongation on the certificate. That is enough to tell a real specification from a part number with the word “Teflon” in the description.
We machine and mould PTFE seals in both virgin and filled grades, and we will tell you when a filled grade is the wrong answer for your chemistry. Send the drawing, the pressure and the fluid, and we will come back with the grade and the forming route, not just a price. Related: back-up rings and gaskets, PTFE rod, tube and sheet stock, y how PTFE parts actually age in service.
Where the Forming Route Meets the Drawing
BOSS Sealing machines PTFE sealing parts from skived sheet, rod and tube, and supplies the filled grades this article works through — glass, carbon, bronze and graphite — as back-up rings, gaskets, washers, guide elements and machined profiles. The stock form and the filler are held to the drawing, so the grain direction and the sinter behind a part can be traced back to the batch it came from.
The questions we ask before quoting are the ones that decide the answer: finished geometry and tolerance, the sealing duty, and whether the part is better cut from sheet or turned from rod. Thin sections often want skiving and thick ones turning, with a stress-relief step between roughing and finishing when the wall is uneven — that is where a quote either holds its flatness or loses it three weeks after the part is on the shelf.
Send a drawing, a 3D model or a sample with the medium, pressure and temperature, and we will come back with the grade, the forming route, the price and the lead time — typically inside 24 hours, with the engineering review at no charge. Write to sales@bosssealing.com o utilice el formulario de contacto.